Best Bending Parts for Precision Metal Fabrication
2026-11-16
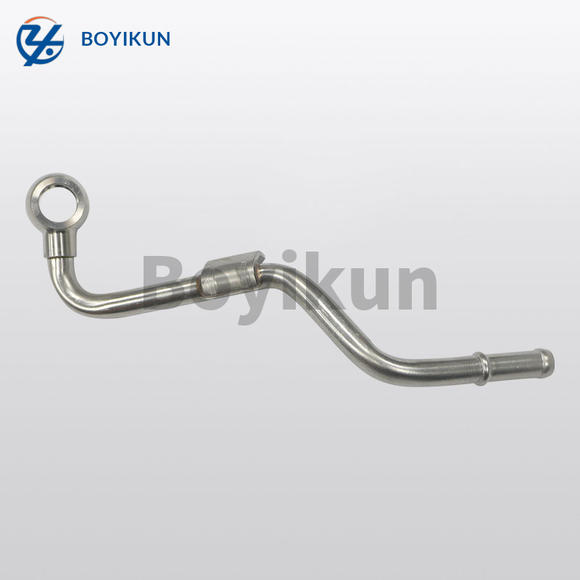
When a bend is off by a fraction of a millimeter, the entire assembly can fail. That’s why choosing the right bending parts for precision metal fabrication isn’t just a detail—it’s the foundation of a successful build. Whether you’re working with stainless steel, aluminum, or exotic alloys, the components you select determine how well your design holds up under stress. At BOYIKUN, we’ve spent years refining our understanding of what makes a bend truly precise. In this blog, we break down the best bending parts that consistently deliver tight tolerances, clean finishes, and long-term reliability—so you can stop guessing and start building with confidence.
Material Choices That Keep Tight Tolerances From Drifting
Selecting the right material is often what separates a dimensionally stable part from one that wanders off spec after thermal cycling. Invar and other low-expansion alloys earn their keep in metrology fixtures and optical mounts, but they're not the only path. For aluminum components, opting for stress-relieved 7050 over 6061 can cut residual stress enough to reduce post-machining warpage by a noticeable margin, especially on thin-walled features.
Polymers present a different challenge. Glass-filled PEEK or Torlon hold their shape far better than unfilled nylons when humidity fluctuates, because moisture absorption is the real tolerance killer in plastic parts. In high-precision assemblies, pairing a ceramic shaft with a hardened steel bushing can keep clearance constant over thousands of cycles, whereas a softer stainless would gall and progressively shift the fit.
Sometimes the smartest material choice isn't the most exotic. Cast iron beds in machine tools remain common because their vibrational damping and thermal mass help resist the micro-movements that accumulate into visible drift. Matching the coefficient of thermal expansion between mating parts, like using a titanium fastener in a carbon fiber structure, can be more effective than chasing a single "perfect" material.
How Grain Direction Changes the Way Parts Bend
When sheet metal is rolled, its internal crystals stretch into elongated grains that run parallel to the rolling direction. Bending across these grains forces them to separate slightly, which makes the outside of the bend rougher and more prone to cracking. Bending along the grains lets the material flow more easily, but it can also cause uneven deformation at the edges.
A part bent perpendicular to the grain typically holds a tighter, cleaner radius without splitting, because the continuous grain lines act like tiny reinforcing fibers. If the same part is bent parallel to the grain, the outer surface may show orange-peel texture or even micro-tears, especially in harder alloys. That is why an inside bend radius often needs to be larger when the bend line runs with the grain.
Practical layouts try to orient critical bends against the grain whenever possible. If a flat pattern forces one bend to follow the grain, fabricators may compensate by increasing the radius, annealing the material, or accepting a slightly weaker corner. The direction of the grain is not just a cosmetic detail; it changes where stress concentrates and how the part eventually fails.
Designing Springback Out Before the First Prototype
Springback rarely announces itself politely. It waits until the first physical tryout, when the die is already cut and the budget is already burning. The smartest teams don't treat prediction as an academic exercise; they treat it as a material property that can be dialed out early. By feeding high-fidelity material data into forming simulations before any steel is ordered, you can map the entire strain path and identify where elastic recovery will fight you. That map becomes your starting point for compensation geometry, not a post-mortem report.
Compensation is not a one-shot correction. It is an iterative loop that should happen entirely on the screen. By adjusting die faces, punch radii, and draw beads in the virtual model, you shift springback from a visible defect into a controlled displacement that the next stamping step can absorb. The key is to optimize for the whole process chain, not just the final panel. A door inner that springs 0.3 mm in the corner might be perfectly fine if the hemming operation naturally pulls it back. That kind of insight only comes when you simulate downstream operations before the prototype exists.
The real victory is not eliminating springback completely, but making it boringly predictable. When every bend, every trim line, and every restrike is evaluated against a tolerance stack early on, the first prototype becomes a validation step rather than a discovery phase. Tooling changes shrink from weeks to days because the digital twin has already absorbed the trial-and-error. Designing springback out before the first prototype means treating the virtual world as the primary workshop, and the physical press as the final confirmation.
Bend Relief Cuts That Prevent Cracks in Hard Metals
Hard metals don’t forgive tight corners. When you put a 90-degree bend in something like 4140 chromoly or hardened stainless, the outside edge of the bend stretches while the inside compresses. At the very ends of the bend line, that tension has nowhere to go except into the sheared edge, which usually carries micro-fractures from cutting. That’s where cracks begin. A bend relief cut—a small slot, notch, or drilled hole right at the end of the bend line—interrupts that stress path before it reaches the edge. Instead of tearing, the material flexes around a defined boundary.
The geometry of the relief matters more than most people expect. A sharp-cornered rectangular notch might seem fine, but those corners become new stress risers and crack anyway. Round or teardrop shapes distribute load along a curve, which hard metals need. Keep the relief width at least one material thickness, and run it slightly past the bend tangent line so the bend doesn’t pinch the relief closed. Laser or waterjet cutting gives clean edges, but even a drilled hole at each bend terminus beats a saw cut with burrs.
If you’re prototyping in annealed stock but the final part will be heat-treated, cut the reliefs first. Hardening after bending seals in residual stress; a relief cut added later can spark cracks at the cut edge. In production, standardize relief diameters to match existing tooling—using the same punch size for piercing and relief holes saves a tool change and keeps edge quality consistent.
Why Thin-Gauge Parts Need a Different Bend Strategy
Thin materials rarely respond to standard bend tables the way heavier plate does. The neutral axis sits closer to the inner surface, but any slight inconsistency in grain orientation, edge burr, or die clearance gets amplified across a long, flexible flange. A setup that works repeatedly on 3 mm stock can produce wavy edges or inconsistent angles on 0.8 mm without any obvious cause.
Springback control also shifts from a tonnage problem to a stability problem. Thin flanges may not push back with much force, but they buckle, twist, or ripple before the bend line fully sets. Holding pads, staged wiping, and smaller punch radii become far more important than increasing pressure. In many cases, adding tonnage makes the distortion worse by driving uneven contact along the bend.
Tooling reuse is another reason a different approach matters. If a shop uses the same die opening and punch radius for a range of thicknesses, the thin parts suffer first. Marks, scratches, and localized thinning near the bend line are common. Choosing the right die gap, polishing contact surfaces, and adjusting bend sequencing for thin material isn't extra work; it's the only way to keep dimensions repeatable without secondary straightening.
Prototyping Methods That Catch Fit-Up Issues Early
A scale mockup cut from scrap plate can expose fit-up gremlins long before the first production weld. On a recent skid frame, a shop knocked together a half-length corner joint from offcuts and immediately saw that the gusset interfered with the diagonal brace. Ten minutes with a grinder fixed the paper drawing; discovering the same clash after full-scale cutting would have cost half a shift.
Digital prototypes help too, but only when the assembly model includes actual fabrication tolerances and not just nominal CAD geometry. One fabricator started running a shrink-wrap check inside the 3D model after every revision, flagging any pair of parts whose combined flatness and squareness tolerances left less than a 3 mm root opening. That simple rule has caught bolt-hole misalignment and bevel gaps on pipe supports, pipe shoes, and vessel clips before the steel ever hits the saw.
For complex interfaces, a quick 3D-printed trial piece gives the crew something to hold against the real frame. It is not about making a pretty model; it is about walking the print around the assembly, feeling where a stiffener blocks a wrench or a flange sits proud of its mating face. Those discoveries are cheap on a Saturday afternoon and brutally expensive during hydrotest.
FAQ
Custom brackets, electronic enclosures, mounting plates, and small clips lead the pack. Their success hinges on repeatable angles and hole locations that stay true after forming.
5052 aluminum and 304 stainless steel are reliable choices because they balance ductility and strength. For very sharp bends, annealed or half-hard tempers reduce cracking at the bend line.
Sequence matters. Bending from the inside out, using laser-cut relief notches, and checking against a fixture after each hit keeps cumulative error low. A CNC backgauge also locks in flange lengths.
One material thickness is a safe rule for most cold-rolled steel and aluminum. If you need a radius smaller than that, switch to a softer temper or accept a higher scrap rate from edge cracking.
Bending shifts metal near the bend zone, so holes drilled before forming can end up oval or out of position. Reaming or boring after bending restores true diameters and exact center-to-center distances.
Bending across the grain allows a tighter radius and cleaner edge. If you must bend parallel to the grain, add 50% to the minimum radius or use cross-rolled material to avoid micro-cracks.
A tight shop can hold ±0.5 degrees on bend angles and ±0.010 inches on flange lengths for parts under 12 inches. Holding anything tighter usually requires in-process angle correction and custom tooling.
CNC press braking with air bending is the sweet spot. It adapts to different materials quickly and, with angle measurement feedback, keeps springback under control without dedicated dies.
Conclusion
Material selection sets the floor for how tight a bend tolerance can actually hold. If you choose a grade that work-hardens unevenly or has inconsistent thickness, even the best tooling will fight you. Pairing the right alloy with its grain direction matters just as much—bending across the grain usually gives cleaner results, while going with the grain invites cracking and dimensional drift. For hard metals, adding proper bend relief cuts at corners or notches stops stress from concentrating where the material wants to tear.
Springback is rarely a surprise if you plan for it before the first cut. Overbending by a calculated amount, or adjusting the die angle to compensate, keeps parts from relaxing out of spec after forming. Thin-gauge stock demands a different approach: lighter tonnage, tighter radii control, and sometimes staged bending to avoid wrinkling. Prototyping with quick-turn methods—like laser-cut blanks and manual press brake setups—surfaces fit-up issues early, before a full production run locks in a costly mistake.
Contact Us
Contact Person: Xianchen Hu
Email: [email protected]
Tel/WhatsApp: 86-13248645200
Website: https://www.hexnb.com/