Custom Roller Conveyor Shot Blasting Machine Solutions for Efficient Surface Preparation
2026-08-15
Most surface preparation problems aren't caused by the abrasive—they're caused by a machine that was never designed for your parts. If you're running a roller conveyor shot blasting line that forces every workpiece through the same fixed blast pattern, you're leaving efficient surface preparation and finish quality on the table. At PuHua, we start with your geometry, your production rate, and your coating requirements, then build the system around them. The result? Cleaner profiles, fewer rework cycles, and a line that actually keeps up with demand. Here's what goes into that kind of custom solution—and why it matters more than you might think.
Contoured Roller Paths Matched to Your Product Mix
Standard straight rollers treat every item the same, but your product line rarely works that way. A contoured path takes the actual shape, weight, and balance of each product into account, so bottles, cartons, or pouches move through curves and merges without twisting, tipping, or colliding. The result is a line that keeps its pace even when you switch from a tall skinny container to a short wide one.
Rather than forcing your product to adapt to the conveyor, the roller profile is machined or molded to cradle specific contact points. This matters most where products change direction or accumulate. When a roller path follows the natural footprint of an item, side pressure drops, scuffing is reduced, and downstream equipment receives items in the right orientation more consistently.
The real advantage shows up during changeovers. Because the contours are matched to the full range of your mix, operators spend less time adjusting guides and rails. A well-designed set of contoured rollers can handle multiple SKUs with minimal intervention, keeping throughput steady without adding complexity to the line.
Blast Intensity Tuned for Thin-Gauge and Thick-Plate Alike
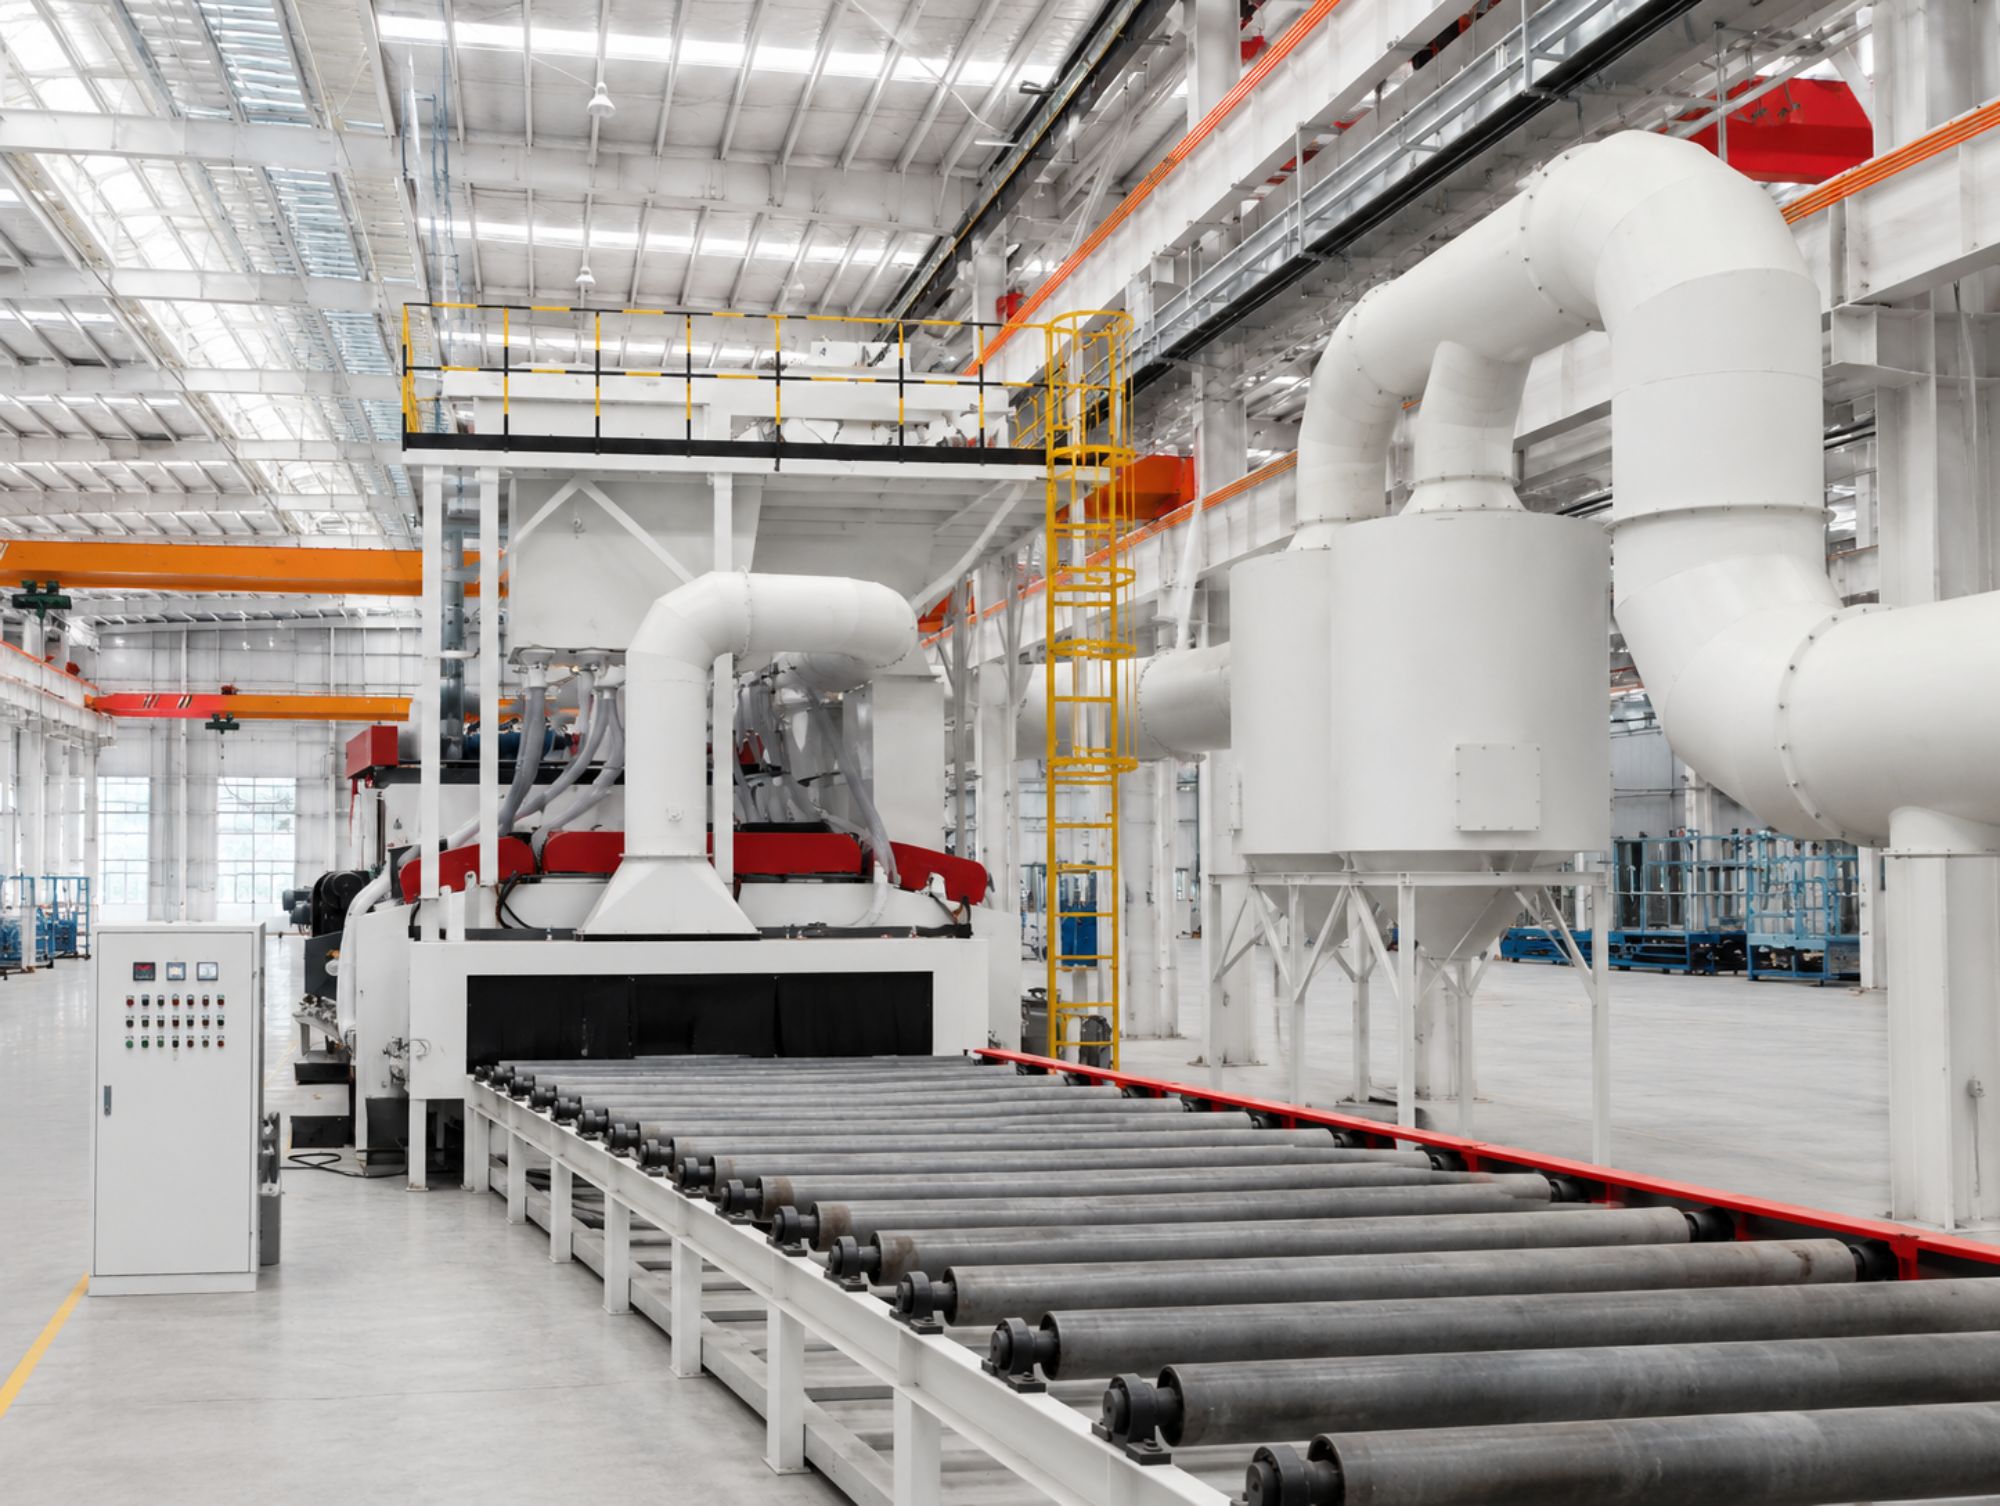
The control cabinet has a small rotary dial that shifts the media/air mix on the fly. Thin-gauge panels get a softer, wider fan so they stay flat; thick plate can be hit with a tighter, faster stream without changing nozzles. It's not just a two-position switch: the adjustment range covers everything from light etch to deep profile work.
Operators tend to mark the dial positions for repeat jobs. A 1/4 turn might drop the pressure enough to keep 0.8 mm sheet from warping, while a full clockwise setting delivers the kind of anchor pattern needed on 12 mm structural steel. The machine doesn't vibrate or surge when moving between extremes.
Because both ends of the range are actually usable, there's less need to keep a separate blasting unit just for delicate work. One person can process mixed-material batches without stopping to reconfigure the hopper or swap out a valve.
Inline Surface Prep That Keeps Pace With Welding Cells
On a busy fabrication line, the gap between weld stations and finishing often becomes the bottleneck nobody planned for. Inline surface prep equipment changes that by mounting directly into the transfer system, so parts move from the torch to a brushing or blasting module without leaving the cell. The result is not just less handling but a surface that is ready for coating or inspection while the next weld is still cooling.
The real test is cycle time. Weld cells run on seconds, not minutes, so surface prep units are built around rapid tool changes and programmable brush pressure. Instead of waiting for a separate grinding booth, operators see mill scale and spatter removed immediately after each pass, with the same robot or conveyor controlling both weld and clean steps.
That kind of synchronization also trims hidden costs. Fewer forklift moves mean less risk of scratches or contamination, and fewer work-in-process racks sitting between departments. For teams already pushing weld travel speeds higher, inline prep keeps the downstream steps from becoming the next constraint.
Sealed Cabinet Design for Cleaner Shop Air
Most cabinet saws look sealed until you trace the airflow. Gaps around the door, an open back panel, or a poorly fitted dust port let fine dust escape before it ever reaches the collector. Sealing the cabinet isn't just about closing holes; it's about creating a controlled path for air and dust.
Start with the cabinet body. Use plywood or MDF and caulk every interior seam, then add closed-cell foam tape around the access door so it compresses evenly when latched. Angle the floor into a hopper that feeds the main dust port instead of leaving a flat bottom where chips pile up. For the blade opening, a brush strip or adjustable throat plate keeps airflow directed downward while still allowing blade changes.
Once the cabinet holds negative pressure, you'll notice less dust settling on nearby surfaces and less haze in the air after long cutting sessions. Check the seals every few months; foam wears out and hinges loosen. A simple smoke test—hold a stick of incense near the seams while the dust collector runs—reveals any leaks worth fixing.
Rapid Retooling for Short-Run Production Schedules
When the order mix shifts weekly, tooling can't stay bolted to one setup. Quick-change fixtures and preset tool offsets let operators swap jaws, stops, and drills in minutes, not shifts. The trick is to treat every changeover as a rehearsal: film it once, time it twice, then cut the wasted motion. Shops that track changeover seconds instead of hours often find they can run three short batches in the time one long job used to take.
Standardized clamping plates help, but only if the toolroom builds them to the same datum every time. A bored locating pin that's off by half a millimeter turns a fifteen-minute swap into an afternoon of chasing taper. Better to invest in a few ground reference blocks and leave the custom fixtures for the jobs that truly repeat. For the rest, a whiteboard sketch and a collet chuck beat a CAD model that never gets updated.
Material staging matters more than the tooling itself. If a short-run order sits waiting for bar stock or inserts, the retooling speed is wasted. Pull kits for the next three jobs before the current one finishes, and keep a shadow board at each machine so nothing gets borrowed without a replacement. Rapid retooling isn't about buying faster equipment — it's about removing every pause that isn't cutting metal.
Long-Life Wear Parts That Lower Cost Per Square Foot
Wear parts often get treated like disposable items, but the math tells a different story. When a blade, liner, or cutting edge lasts twice as long, the cost per square foot doesn't just drop by half—it falls further because you also skip the downtime, labor, and replacement overhead that come with frequent swaps. Choosing materials like tungsten carbide, hardened alloys, or ceramic composites shifts the expense from recurring purchases into a one-time investment that keeps paying for itself month after month.
The real savings show up in high-abrasion environments where softer parts might need changing every few weeks. A long-life wear component with a slightly higher upfront price often ends up costing 40-60% less per square foot over a year, simply because the machine keeps running instead of sitting idle for maintenance. That's the kind of number facility managers notice on the quarterly budget, and it's rarely talked about in typical product sheets.
Field data from aggregate plants and recycling yards shows the same pattern: swapping to wear parts rated for extended service intervals reduces both direct procurement and indirect labor costs. The per-square-foot metric becomes the easiest way to compare options—not just the sticker price of a part, but what it actually costs to process each square foot of material over the life of the machine.
FAQ
These systems are commonly used for long steel sections, plates, pipes, and welded fabrications that can rest on powered rollers. You also see them handling structural beams, angles, and heavy castings where a continuous pass is more practical than batch tumbling.
Slower travel gives the abrasive more contact time, which helps remove deeper scale or stubborn rust. Faster speeds push more parts through the line but can leave uneven cleaning if the blast pattern or abrasive flow isn't fine-tuned for that rate.
Yes. The turbine speed, abrasive flow, and sometimes the angle of the blast wheels can be modified. For thin or heat-sensitive parts you reduce the intensity and maybe use a finer abrasive, while heavily scaled steel requires a more aggressive setting.
Regularly check the roller bearings for abrasive ingress, inspect blast wheel blades and liners for wear, and keep the abrasive recovery and separator system clean. You also need to monitor the dust collector filters and empty the hopper before abrasive fines build up.
Look for full enclosure with interlocked access doors, emergency stop pulls along the conveyor, proper ventilation to control dust, and light curtains or barriers at the entry and exit openings. Abrasive ricochet containment and noise dampening are also important for operator safety.
Consider your maximum workpiece width and height, conveyor load capacity, and whether you need special in-feed or out-feed handling. If your parts have odd protrusions, heavy weight distribution, or require multiple blast angles, a custom layout usually pays for itself with fewer passes and less rework.
Steel grit and steel shot are the most common because they hold up well and can be recycled many times. Grit cuts faster and leaves an angular profile for coating adhesion, while shot peens and smooths the surface. Many shops use a mix of both to balance cleaning speed with final roughness.
It often includes variable speed control, adjustable blast wheel positioning, and quick-change abrasive settings. Some systems use recipe-based controls that store parameters for different part types, so the operator can switch from one job to the next without a full mechanical adjustment.
Conclusion
A well-matched roller conveyor shot blast system does more than strip mill scale or profile a surface—it becomes a quiet production partner. When the roller paths are contoured to follow the actual mix of profiles, tubes, and plate your shop runs, there is no need to constantly hand-position awkward parts. The blast intensity can be dialed in for thin-gauge sheet without warping or cranked up for heavy plate that demands a deeper anchor profile. That flexibility means the same line can feed a robotic welding cell with consistently clean, ready-to-weld material, keeping the entire fabrication flow moving at the pace your automation sets.
The cabin itself is sealed to keep fine dust and abrasive from drifting into the rest of the shop, which matters when the machine sits near other operations. For shops juggling short-run schedules, tooling isn't a week-long headache—roller spacing, blast angle, and masking can be switched over quickly between part families. Underneath all of that, the wear parts are selected and arranged to survive the daily grind, spreading abrasive contact across replaceable zones so cost per square foot stays predictable. The result is not a generic blasting cabinet, but a surface preparation line shaped around your throughput, your part mix, and the air quality your floor deserves.
Contact Us
Contact Person: Bruce
Email: [email protected]
Tel/WhatsApp: +86 15166629468
Website: https://www.povalchina.com/