Metal Tags Factory: From Raw Metal to Finished Custom Tags
2026-10-01
Ever wondered how a raw sheet of metal transforms into the custom tag on your favorite product? At Kingming, we turn that curiosity into craft—cutting, stamping, and finishing each tag with precision that speaks for itself. This isn't just about tags; it's about the journey from industrial blank to branded detail, and we're pulling back the curtain.
Choosing Raw Metal That Holds Up
Raw metal selection often gets reduced to a quick glance at a spec sheet, but the reality is more about matching the alloy's failure modes to the stresses it will actually face. A steel that excels in a controlled indoor setting might crack within months when exposed to temperature swings or mild chemical contact, so it pays to look beyond tensile strength and consider how the grain structure responds to repeated loading.
For components that need to hold up over years of service, pay close attention to corrosion behavior in the specific environment—not just the generic rating. A stainless grade that handles salt spray fine may still pit under constant condensation mixed with industrial dust. Asking suppliers for real-world performance data from similar applications gives you a better read than a polished datasheet ever will.
Also think about how the metal will be joined or finished. A high-hardness alloy that resists wear beautifully can become a nightmare to weld without introducing microcracks, and those small flaws often become the starting point for premature failure. Sometimes the smartest choice isn't the strongest metal on paper, but the one that tolerates your entire manufacturing process without losing its edge.
Cutting Blanks Without Losing the Grain
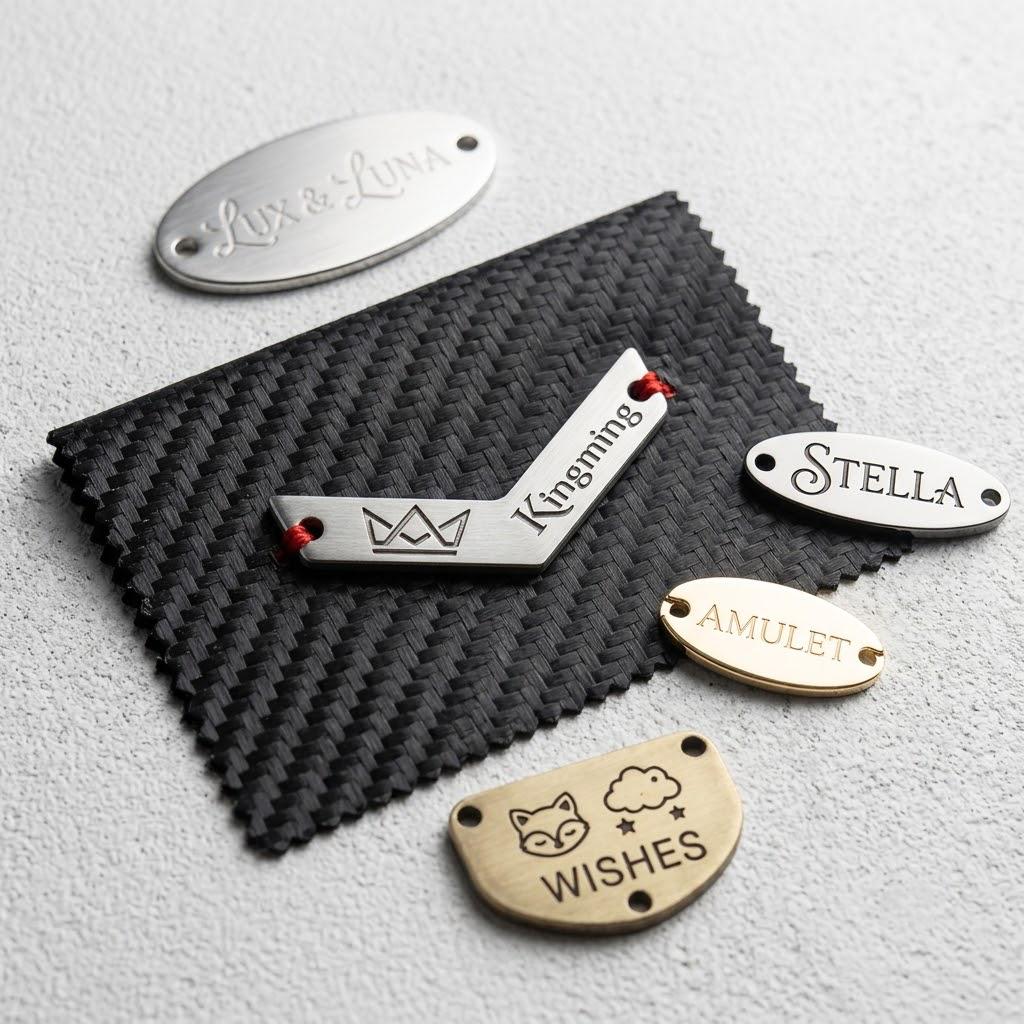
When you cut a blank from a larger board, the grain direction isn't just a visual detail—it decides how the piece will move, sand, and take a finish. Mark the end grain with a pencil before you make the first cut, and reference that mark at every step. If you lose track, you can usually read the grain by wetting the surface slightly or looking at the side of the board where the lines run tightest.
A common mistake is slicing the blank to size without considering how the grain flows through the profile. If the blank is for turning, aligning the growth rings so they run parallel to the lathe axis makes a stronger, cleaner result. For flat work, keep the long edges running with the main grain direction rather than across it. This reduces tearout and keeps the piece stable when humidity changes.
There's no need to overthink it, but a few slow seconds spent studying the board before cutting saves real frustration later. Trace the intended blank shape onto the wood, then adjust its position slightly if the grain lines would exit through a thin section or a short edge. Sometimes rotating the template a few degrees is all it takes to keep the grain running the full length of the piece.
Etching Fine Details That Stay Legible
Fine detail work lives or dies by tool control and material choice. When lines get thin, depth consistency matters more than raw precision. A slightly shallower cut in a dense alloy can vanish under finish, while the same pass in softer stock leaves a crisp, readable groove. Testing on scrap with the exact coating or patina you plan to use saves hours of guesswork.
Legibility also comes down to contrast, not just line width. A perfectly etched 0.2 mm letterform fails if it blends into surrounding texture. Adjusting angle, pulse frequency, or etch depth to create a subtle shadow or brighter facet can lift fine text without making it bolder. Think of it as sculpting light rather than simply removing material.
Cleanup is the step most often rushed. Micro-burrs and residue accumulate in tight corners and close counters, filling gaps that should stay open. A soft brush, low-pressure air, or a gentle solvent pass restores the original stroke width. Let the part cool before handling, and inspect under magnification at the same angle as the final viewing position.
Finishing Surfaces for Long-Term Wear
Achieving surfaces that hold up under continuous abrasion, sliding contact, or repeated impact goes far beyond applying a simple protective coat. The finishing process must address the microscopic terrain of the material, where high points concentrate stress and low points can trap debris that accelerates wear. Methods like precision grinding and lapping create a flatter, more uniform surface, which reduces localized pressure and gives any subsequent coating a better foundation. At the same time, treatments such as shot peening introduce beneficial compressive stress that slows the initiation of fatigue cracks along load-bearing edges.
For harder working environments, depositing a thin film with superior hardness or low friction can dramatically extend service life. Physical vapor deposition (PVD) is often used to apply titanium nitride or diamond-like carbon layers, which are only a few microns thick but alter how the surface interacts with mating parts. These coatings perform best when the underlying substrate has been properly prepared—cleaned, de-burred, and sometimes heat-treated to the right core hardness—so the hard outer layer does not collapse under load. In applications involving both wear and corrosion, duplex treatments that combine nitriding with a sealed topcoat offer a more reliable barrier than either step alone.
No single finishing recipe works for every wear scenario. Abrasive wear from hard particles calls for high surface hardness and minimal porosity, while adhesive wear between sliding metals may respond better to lowering friction through a solid lubricant or a polished oxide layer. Consulting wear maps or conducting controlled wear tests early in the design phase helps identify whether the dominant failure mode is scratching, pitting, or material transfer. Once that is known, the finishing sequence—from initial machining to final coating and even post-coat polishing—can be tuned to match the exact service conditions, often yielding a component that outlasts an off-the-shelf alternative by a wide margin.
Proofing Custom Designs Before Cutting
Before you commit a custom design to expensive material, run a scaled-down proof on an offcut. Watch how the beam or bit handles tight corners and thin bridges. If a section feels fragile in your hand, it will likely fail during cutting or assembly.
For layered pieces or interlocking tabs, a physical test in cardboard or scrap acrylic saves more time than adjusting vectors on screen. Stack the cut layers exactly as you plan to assemble them and check that every slot lines up without forcing. A slight shift in kerf or material thickness becomes obvious once the parts are in your hands.
Fine text and decorative details demand a separate check at actual size. Reduce power or speed for a first pass, then inspect the edges under good light. Small counters and reverse-cut elements often need more spacing than the file suggests, and a single proof tells you where to open up the geometry before the final cut.
Final Checks Before Tags Leave the Floor
Before a single hangtag or care label makes its way into a shipping carton, the team runs through a tight physical checklist at the packing station. Every printed barcode gets scanned against the order manifest, and any tag with a smudged price or a slightly off-center fold is pulled from the line. A quick rub test on the ink, a tug on the attachment loop, and a side-by-side color check against the approved sample are all done in under ninety seconds per batch.
What often gets missed in digital proofs shows up here under the warehouse lights: a batch number that shifted during cutting, a QR code that scans to last season's product page, or a thread color that looked neutral on screen but reads green against the actual garment. Only after the shift lead signs off on the final count and the rejected pile is logged does the tag tray move toward the dock.
FAQ
Common options include aluminum for its light weight and corrosion resistance, brass for a classic gold-like appearance, stainless steel for strength in harsh environments, and copper when you want a warmer reddish tone that develops a natural patina over time.
It starts with cutting blanks to the required shape, then moves into marking or etching the design, followed by surface finishing such as polishing, brushing, or plating. Finally, any protective coating or color fill is applied before inspection and packaging.
Yes, most factories accept custom dimensions and die-cut shapes. You only need to provide a vector file or detailed drawing, and they can produce everything from tiny round tags to large rectangular plates with holes or slots for fastening.
The most common methods are chemical etching for fine detail, laser engraving for permanent high-contrast marks, and stamping for deep impressions. Each technique suits different materials and design complexity.
Depending on the metal and finish, they can withstand UV exposure, moisture, salt spray, and temperature swings. Stainless steel with a clear protective layer is often chosen for extreme conditions, while anodized aluminum works well for moderate outdoor use.
You can add color infill, barcode or QR codes, serial numbers, adhesive backing, holes, slots, or chain attachments. Surface finishes like matte, gloss, brushed, or antique effects also change the final look.
Many factories offer flexible runs, but the minimum often depends on the process. Laser engraving can be cost-effective for small batches, while chemical etching or stamping may require a higher quantity to justify setup costs.
Each batch is usually checked for dimensional accuracy, edge smoothness, marking clarity, and finish consistency. Some factories also perform adhesion tests for coatings or readability tests for barcodes to ensure the tags meet the agreed specifications.
Conclusion
In a metal tags factory, the journey starts long before any machine fires up. We hand-pick raw stock—stainless steel, brass, or aluminum—based on where the tag will live and how much abuse it will take. A tag bolted to outdoor equipment doesn't get the same alloy as one inside a climate-controlled lab. Once the right metal is chosen, blanks are cut with a focus that borders on obsessive: the grain direction matters. Cutting against the grain can leave edges that fray or weaken under stress, so every sheet is oriented before the blade comes down. Then comes etching, where fine details—serial numbers, barcodes, tiny logos—are carved into the surface. The depth and speed are tweaked so the marks stay legible even after years of rubbing, washing, or sun exposure.
After etching, the surface gets a finish built for long-term wear. That might mean a brushed texture to hide scratches, a powder coat for chemical resistance, or a clear sealant that keeps ink from fading. But before any of this happens to a customer's order, a proof is sent out—a digital or physical sample that shows exactly how the design will look after cutting and etching. The customer signs off, and only then does production begin. On the floor, the final checks are a mix of measuring, testing, and plain old looking. A tag that's off by half a millimeter or has a slightly blurred character gets pulled. It’s not enough to make tags that look right on day one; they have to look right on day five hundred.
Contact Us
Contact Person: Jamie Zeng
Email: [email protected]
Tel/WhatsApp: +86 13728219269
Website: https://www.kmhardware.com