Top Giant Press Brake Machines for Heavy-Duty Metal Fabrication Needs
2026-10-15
If your shop regularly takes on jobs with thick plate, long beams, or heavy structural sections, you already know a standard press brake won’t survive the workload. The machines that handle this kind of punishment are a different breed entirely—giant, powerful, and built for the long haul. This article breaks down the top contenders in that class, and one name that keeps coming up in serious fabrication circles is HUNSONE.
What Really Happens When You Push a Standard Brake Too Far
Standard brakes handle everyday stops without complaint, but when you lean on them hard for repeated high-speed braking or a long downhill run, the heat buildup quickly outpaces the cooling design. The friction material in the pads relies on a resin binder that starts to break down around 600–700°F. As that resin vaporizes, a thin cushion of gas forms between the pad and rotor, so pressing the pedal feels mushy and the car just doesn't shed speed the way it did a few corners ago. You might also catch a sharp, acrid smell and see a bluish tint on the rotors after you stop.
If you ignore that warning and keep pushing, the fluid itself becomes the weak point. Standard brake fluid absorbs moisture over time, and under sustained heat that water boils into vapor inside the lines. Because vapor compresses easily, the pedal can suddenly sink toward the floor while braking force drops to almost nothing—not a gradual fade, but a near-total loss right when you need it most. The rotors may also develop hairline cracks from thermal stress, and the pad surface can glaze over, making even normal stops feel slippery and unresponsive.
After a session like that, the brakes won't simply cool down and return to normal. Glazed pads and heat-cycled rotors usually need replacement or resurfacing, and the boiled brake fluid must be flushed because its boiling point has permanently dropped. Standard brake hardware is built for predictable street loads, not the sustained abuse of track laps or aggressive mountain descents.
The Hidden Cost of Frame Flex in Heavy Plate Work
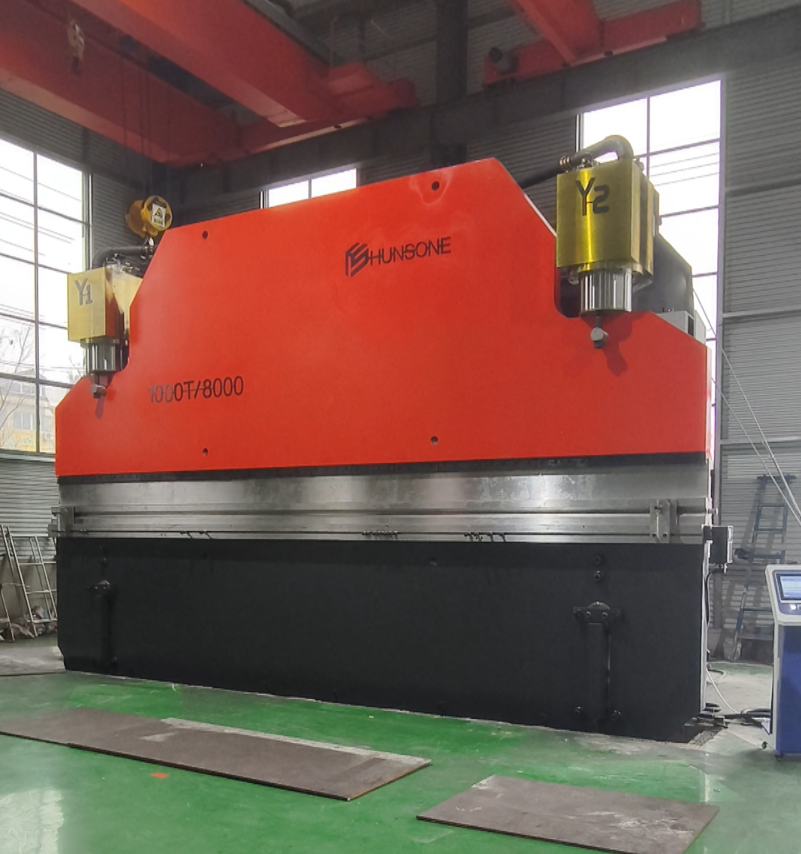
Frame flex is rarely the first suspect when a heavy plate job drifts out of tolerance, yet it quietly erodes margins on nearly every oversized part. A gantry or bridge that bends a few thousandths under a multi-ton load may still cut, weld, or drill, but the tool path no longer matches the digital model. Operators compensate with slower feeds, extra finishing passes, or manual shimming—each one adding hours that never appear on the quote.
The expense compounds because deflection is not a one-time failure; it returns with every cycle, wearing inserts unevenly, stressing linear rails, and forcing repeated setup checks. Shops that track scrap often find that a significant share of rejected plates trace back to the same flex-prone station, not to bad material or programming errors. Over a year, the cost of rework, expedited replacements, and shortened spindle life can far exceed the price of a stiffer frame or a retrofit damping system.
Addressing the issue starts with measuring actual deflection under load rather than trusting static specifications. Simple dial indicators placed at mid-span during a heavy cut reveal how much the structure moves. From there, targeted bracing, thicker cross-sections, or even repositioning the workpiece can bring the numbers down. The payoff shows up quickly: less hand fitting, fewer scrapped plates, and a floor that no longer waits on a machine fighting its own skeleton.
Why Backgauge Accuracy Matters More at Full Tonnage
At full tonnage, every fraction of a millimeter in backgauge positioning translates directly into bending force distribution. When the press reaches maximum pressure, the sheet metal has nowhere to go except where the backgauge dictates. A slight misalignment that would be harmless at half load can turn into a visible angular error or even material cracking, because the full force amplifies any dimensional inconsistency across the bend line.
The backgauge acts as the reference plane for the entire forming operation. Under lower pressures, the material can absorb small positioning errors through elastic deformation or slight sheet slippage. But once you hit the machine's rated tonnage, that forgiveness disappears. The workpiece is pressed firmly against the stops, and any deviation in backgauge parallelism or squareness gets stamped directly into the final part geometry.
Operators who routinely run jobs near maximum capacity know that backgauge repeatability becomes non-negotiable. A backgauge that drifts by even 0.1 mm can produce a stack of parts with visibly inconsistent flange lengths. At full tonnage, the cost of rework or scrap rises sharply, making accurate backgauge setup not just a quality concern but a direct driver of shop profitability.
Hydraulic Systems That Don't Overheat on Long Runs
Long-haul machinery pushes hydraulic fluid through countless cycles, and heat builds up when components can't shed it fast enough. Overheated oil thins out, seals degrade, and pumps start to whine under the strain. The fix starts with sizing the reservoir right — too small and the fluid never gets a chance to cool and release trapped air. Pair that with a well-placed heat exchanger, either air-blast or water-cooled, and you've already cut peak temperatures by a wide margin. Many operators overlook the return-line filter; a clogged one forces the pump to work harder, adding unnecessary thermal load. By keeping the filtration path clean and the oil viscosity stable, the system runs cooler even when the job stretches into double shifts.
Component choice matters just as much as cooling hardware. Piston pumps with case drain lines routed directly back to the tank, rather than through a restrictive manifold, reduce internal churning losses that quietly cook the fluid. Variable-displacement pumps help too — they only move the oil the work demands, instead of constantly recirculating at full flow. Hose routing plays a subtle role: keep high-pressure lines away from the reservoir and avoid sharp bends that create localized restrictions. On long runs, every degree saved in the plumbing shows up as lower bulk oil temperature hours later.
Finally, monitor the system's health with a temperature gauge placed at the tank return, not just at the pump outlet. A return-line reading tells you how much heat the entire circuit is actually retaining. If the needle climbs past 140°F on a long grade, it's time to check for internal leakage across cylinder seals or a relief valve that's cracking too early. Those hidden leaks convert horsepower straight into heat without doing useful work. With smart fluid conditioning, honest component selection, and a watchful eye on return temperatures, hydraulic systems can grind through marathon sessions without ever hitting the red zone.
Changing Tools on a Giant Brake Without the Usual Headache
The worst part of swapping tooling on a large brake isn't the weight, it's the alignment. You can have all the lifting gear in the shop, but if the punch and die aren't seated square against the ram and bed, you'll fight uneven bends all afternoon. Start by cleaning the clamping surfaces with a stiff brush and a rag before anything else. Those tiny steel slivers and dried grease do more to make a tool change miserable than the size of the machine.
Use the brake's own hydraulic or mechanical clamping where it exists. On older giants without quick-change clamps, a pair of guide pins or a home-made alignment bar from scrap round stock saves a lot of prying. Slide the upper tool in from the end, keep one hand on the heel to feel the seat, and only then snug the clamp bolts in a crisscross pattern. Never hammer directly on a hardened punch unless you want a chipped edge.
Finally, test the alignment with a thin strip of brass or aluminum across the die opening before you run a real part. Lower the ram just enough to kiss the shim, then check for even indentation. If it's uneven, back off and loosen only the tight side before reseating. That two-minute check turns an hour-long wrestling match into a predictable routine, even on the biggest brake in the shop.
Safety Features That Don't Slow Down Experienced Operators
Experienced operators often resent safety mechanisms that force them to pause, confirm, or bypass routine steps. The best designs remove that friction. Guards that swing clear without tools, interlocks that read intent rather than requiring a hard stop, and sensors that only intervene when a real hazard exists all let skilled hands keep their rhythm.
For instance, a table saw brake can distinguish between a finger and wet lumber, so it won't trigger on every knot. A forklift stability system can ease speed around a corner without cutting power abruptly. These aren't nanny features; they're background helpers that stay quiet until needed.
What matters is that safety doesn't become another task. A good system disappears into the machine's behavior, giving the operator full speed and control in normal conditions while still catching the rare mistake. That balance is what separates equipment people enjoy using from equipment they fight.
FAQ
It usually comes down to bending length and tonnage. Once you move beyond roughly 20 feet of bed length or 1,000 tons of force, you're in territory where standard machines struggle and a purpose-built giant press brake becomes necessary. The frame, crowning system, and back gauge all have to be engineered for that scale.
Hydraulic systems handle sustained high force more gracefully. Electric brakes are efficient and fast at lower tonnages, but when you're pushing 600 tons or more repeatedly, hydraulics give you the control and durability without overtaxing the drivetrain.
Look for a monolithic welded frame with deep side housings and a thick bed and ram. The throat depth also matters—too shallow and you can't bend large plates with flanges. Stress-relieved construction is a must, otherwise the frame can micro-shift under load and ruin repeatability.
You need a good crowning system, preferably CNC-controlled and tied to the actual load. Mechanical shims can work on shorter machines, but on a giant brake, the deflection curve is never linear, so active crowning with multiple hydraulic cylinders under the bed gives the best straightness.
Yes, tooling weight and segmentation become major issues. A 30-foot upper punch can weigh several tons, so quick-clamping systems and overhead cranes are often built into the workflow. Also, using sectionalized tooling lets you swap worn segments without replacing the entire length.
Light curtains alone aren't enough. Large brakes need laser or camera-based guards that can handle long spans, plus mechanical stops and safe-distance calculations that account for the huge inertia after the ram stops. Two-hand controls and proper lockout procedures for die changes are also critical.
It's a direct formula: force equals material tensile strength times thickness squared times length divided by die opening. For heavy plate, you often need a die opening 8 to 10 times the material thickness, which lowers the required tonnage but increases the inside radius. On giant brakes, the bending length drives the tonnage up quickly.
These machines can weigh over 100 tons, so you need a reinforced concrete pad, often 3 to 5 feet thick depending on soil conditions. Vibration isolation pads or anchoring bolts are common, and you need to consider crane access for installation and future maintenance.
Conclusion
When a shop pushes a standard press brake beyond its rated capacity on heavy plate, the failure is rarely sudden. Instead, you get a ram that no longer returns parallel, cylinder seals that start weeping, and a bed that takes a permanent set. That slow degradation compounds the hidden cost of frame flex: on long beds under full tonnage, the center of the ram deflects upward while the ends hold, so the bend angle varies across the workpiece. For thick plate, even half a degree forces shimming, recutting, or scrapping the part. Top giant press brakes attack this with deeper beds, heavily ribbed side frames, and crowning systems that adjust automatically based on load. But frame rigidity is only half the story. At full tonnage, backgauge accuracy often falls apart because the gauge mounts to the floor or a separate rail that shifts under stress. Better designs tie the backgauge directly to the lower beam or compensate electronically so repeated hits land within a few thousandths. Hydraulics also matter on long runs: standard systems heat up, thin out the oil, and slow the ram, adding seconds to every cycle. Heavy-duty machines use oversized reservoirs, oil coolers, or servo-pump drives that hold temperature within a narrow band, keeping cycle times predictable over an eight-hour shift.
Tool changes on a giant brake are where downtime hides if you still wrestle with manual clamps and alignment pins. Quick-clamp systems with hydraulic locking and self-aligning upper tools cut changeovers from twenty minutes to under three, and they eliminate the usual headache of re-zeroing the backgauge after every swap. Safety needs to keep pace without annoying skilled operators. The best giant brakes use laser light curtains that mute during fast approach but react instantly at bending speed, so a veteran can work at full pace without disabling a guard. Two-hand controls and foot pedals are placed for natural body position, not bolted on as an afterthought. When a standard brake is pushed too far, you eventually lose the frame straightness and hydraulic integrity that these safety and precision systems depend on. Choosing a purpose-built heavy-duty press brake means you stop fighting the machine and start trusting it—on the first part, the hundredth, and the ten-thousandth.
Contact Us
Contact Person: James Chen
Email: [email protected]
Tel/WhatsApp: 86 13770803946
Website: https://www.hunsone.com/